
 English

Diagnosis Before Disassembly
A chemical pump fault is cheaper to diagnose than to guess at. The same symptom, low flow, rising vibration, a wet floor under the pump, can spring from a dozen causes scattered across the suction line, the pump, the motor, and the system, and the mechanic who opens the pump before narrowing the list usually replaces the wrong part first. Effective troubleshooting works from the symptom outward: read the evidence the pump is already giving, isolate the system section that owns the cause, and only then reach for tools. This guide sets out the safety preparation that comes before any inspection, a master table mapping the nine most common symptoms to their probable causes and step-by-step fixes, and the diagnostic habits that separate a ten-minute diagnosis from a day of unnecessary disassembly.
Before You Begin: Safety Without Exception
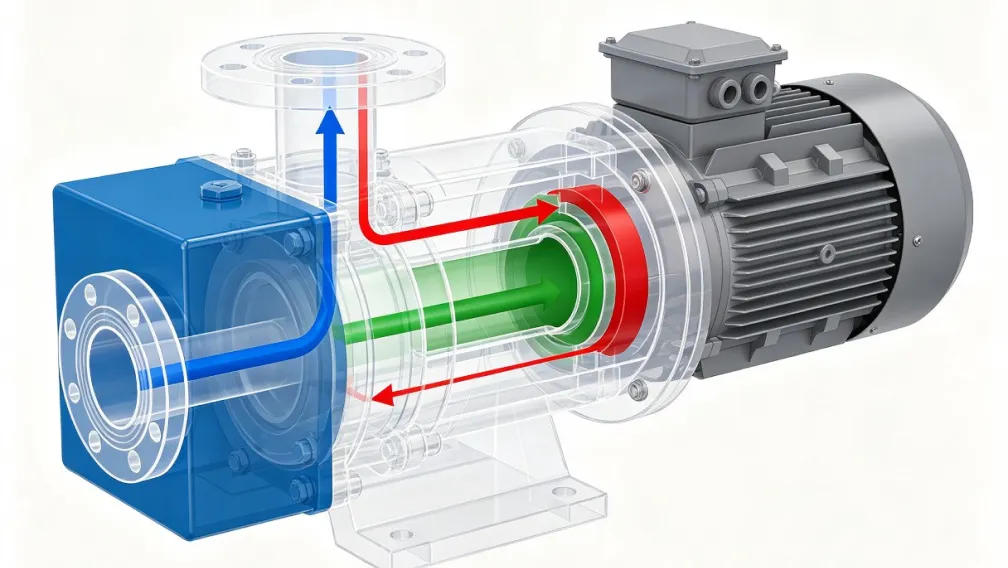
Chemical pumps move hazardous fluids, and every troubleshooting session starts with the same preparation, regardless of how minor the fault seems. Isolate the pump electrically with lockout and tagout, and close both suction and discharge valves. Depressurize, drain, and flush the casing with a liquid compatible with the process before opening any wetted component. Wear the PPE specified for the actual medium: acid suit, face shield, gloves, and respiratory protection where the fluid is volatile. Two hazards deserve explicit warning. A magnetic drive pump can retain process liquid in its containment shell cavity even after the casing appears drained, so internal surfaces are treated as wetted until proven otherwise. And no pressurized casing or shell cavity is ever opened before it is confirmed depressurized and drained. These steps cost minutes; skipping them is how routine inspections become injuries.
Master Troubleshooting Table
The table below maps the nine symptoms that account for the large majority of chemical pump faults to their probable causes and ordered fixes. Work the causes in the order listed; they are arranged from most common and easiest to verify to least accessible.
| Symptom | Probable causes | Step-by-step solution |
|---|---|---|
| No flow on startup | Pump not primed; suction valve closed; reversed rotation; blocked impeller or suction line; lift beyond rating | Confirm suction valve open and casing filled and vented. Bump motor and verify rotation against the casing arrow. Check suction lift against rating, derated for fluid density. Open casing and clear impeller or strainer blockage. |
| Low flow or low pressure | Worn impeller or lining; discharge throttled; suction air ingress; system head above rating; wrong speed; partial cavitation | Compare valve position and system head against the curve. Confirm motor speed matches duty. Hunt suction-side air leaks at flanges and gaskets. Check NPSH margin. Inspect impeller and lining for wear. |
| Low discharge pressure | Wrong rotation; worn impeller; air in casing; system leak; low speed | Confirm rotation. Re-prime and vent. Gauge impeller diameter and wear. Verify motor speed and supply voltage. |
| Vibration or noise | Misalignment; worn bearings; impeller imbalance or erosion; cavitation; loose foundation; solids in impeller | Re-align and re-verify after thermal growth. Check grout and hold-down bolts. Inspect bearings by noise and temperature. Balance or replace an eroded or fouled impeller. Address cavitation on the suction side. |
| External leakage | Worn or dry seal faces; O-ring failure; flange misalignment; cracked lining at flange; gasket failure | Locate the source: seal, flange, or gasket. For seal leaks verify flush flow and replace faces as a set. For flange leaks relieve pipe load, re-align, replace the gasket, torque to spec. Damaged lining turnouts go to relining. |
| Overheating, pump or motor | Running at shut-off or far from BEP; blocked flush; bearing failure; eddy-current heating on metal-shell magnetic pumps; over-greasing | Open the discharge toward the duty point; never run against a closed valve. Restore flush flow. Check bearings and lubricant quantity. On magnetic pumps check shell temperature and fluid suitability. Reduce duty if the motor nears nameplate current. |
| Motor trips or overcurrent | High SG not accounted for; mechanical rub or solids lock; run-out past curve end; bearing seizure; high viscosity; misalignment | Compare actual SG and duty against motor rating. Check for rub and clear solids. Throttle discharge off the run-out. Inspect bearings and alignment. Verify viscosity is within pump limits. |
| Dry-running damage | Loss of suction; started dry; blocked suction; magnetic pump sleeve bearings run dry | Stop immediately and lock out. Restore suction and clear blockages. Inspect seal faces, or sleeve bearings and containment shell on magnetic pumps, for scorching; replace damaged parts before restart. Fit low-flow or dry-run protection. |
| Cavitation noise, gravel-like rattling | Insufficient NPSH; suction line too small or long; clogged strainer; high fluid temperature; throttled suction valve | Open the suction valve fully and clean the strainer. Raise the liquid level or lower the pump. Enlarge or shorten the suction line. Lower fluid temperature where feasible. Throttle the discharge slightly to move out of the cavitation zone. |
| Magnetic decoupling | Excessive torque from high viscosity or density, solids, or blocked discharge; overheated or weakened magnets; oversized impeller | Stop the motor immediately; a decoupled coupling overheats and demagnetizes. Let it cool. Identify and clear the overload cause. Restart; if it decouples again, verify impeller size and fluid properties against rating. Repeated decoupling means weakened magnets: replace the coupling. |
Reading the Symptoms Like a Diagnostician
Three habits make the table work in the field. First, interrogate the history before the hardware: a fault that appeared gradually over weeks points to wear, while one that appeared after an event, a shutdown, a valve operation, a batch change, points to that event. Second, localize before opening: pressure gauge readings, motor current, and sound narrow the cause to a system section, and the section tells you whether the problem is suction-side, pump, or discharge-side before a single bolt is turned. Third, change one thing at a time and record it: the pump's maintenance log and commissioning baseline are what turn a confusing symptom into a confirmed cause, and every corrective action belongs in the same record.
When the Table Is Not Enough
Some faults deserve deeper treatment than a table row allows, and each has its own logic. Mechanical seal leakage follows a five-cause sequence from lost flush to O-ring incompatibility. Magnetic drive pumps have their own failure pair, dry-running and decoupling, both capable of permanent damage in seconds. Self-priming failures trace to five causes from an empty reservoir to reversed rotation. Slurry pump blockages divide between solids overload, line settling, and wear-induced imbalance. And lining wear in fluoroplastic and UHMWPE pumps is a managed condition with its own inspection and relining discipline. These are covered in dedicated guides; the master table points to them when the first-pass fix does not hold.
The Faults That Keep Coming Back
A fault repaired twice is telling you the diagnosis stopped at the component. Recurring failures follow recognizable patterns, and each pattern points past the part to the system. Seal faces that fail every few months are reporting their environment: a flush that intermittently blocks, an alignment that drifts with temperature, or a duty point that has wandered from the best efficiency point. Bearings that fail repeatedly on one pump while identical pumps run clean are reporting that pump's alignment, foundation, or operating point, not a bad batch of bearings. Lining pinholes that reappear after relining are reporting a material mismatch or a thermal abuse pattern, not defective linings. And couplings that decouple more than once are reporting an overload the process keeps generating, not weak magnets alone. The corrective question in every recurring case is the same: what condition keeps producing this failure? Answering it usually requires the operating data and maintenance history rather than another replacement part, and it is the point where manufacturer involvement pays for itself fastest.
Conclusion
Troubleshooting a chemical pump is a discipline of evidence: prepare safely, read the symptom against the probable causes in order, localize before disassembly, and record everything against the pump's baseline. The master table above covers the nine symptoms behind most field faults across sealed centrifugal chemical pumps, magnetic drive pumps, and UHMWPE slurry pumps. When a fault survives the first-pass diagnosis, or when the same fault keeps returning, the cause is usually systemic rather than component-level, and that is the point to involve the manufacturer. Send YFTEL your symptom description, operating data, and maintenance history, and our engineers will work the diagnosis with you.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.