
 English

A corrosion-resistant chemical pump is a significant investment in safety and uptime. The materials and construction that make it survive aggressive media also impose specific care obligations: linings must be inspected for wear, magnetic-drive sleeves must be kept wet, and seals must be flushed correctly.
This guide covers the full maintenance lifecycle, from first installation through annual overhaul, so that a correctly specified pump also becomes a long-lived one.
Installation Best Practices
Most premature pump failures originate not in the pump but in its installation.
Three areas demand attention:
Foundation
Mount the pump on a rigid, level concrete base of adequate mass to absorb vibration.
Grout the baseplate fully (no hollow voids) and allow curing before final alignment.
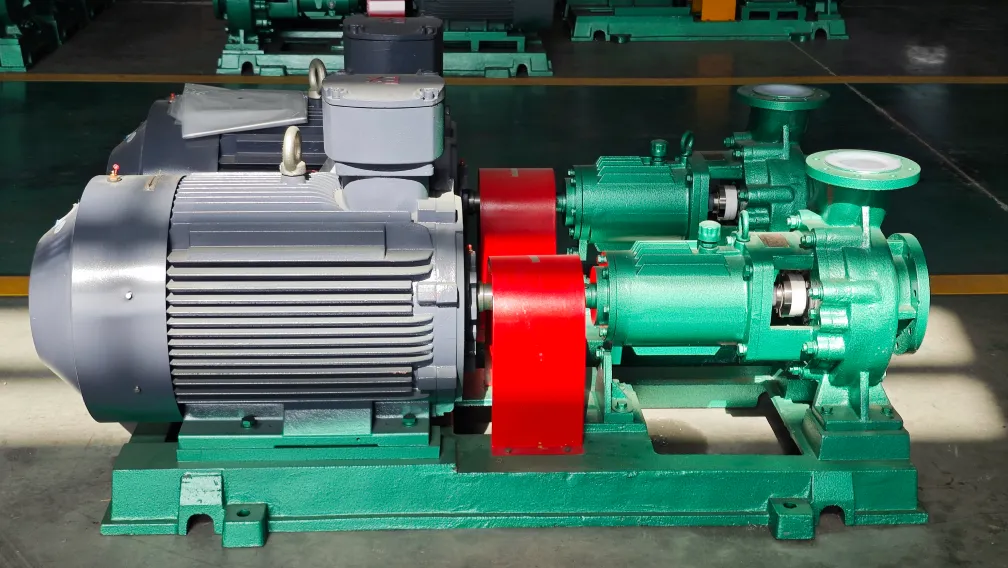
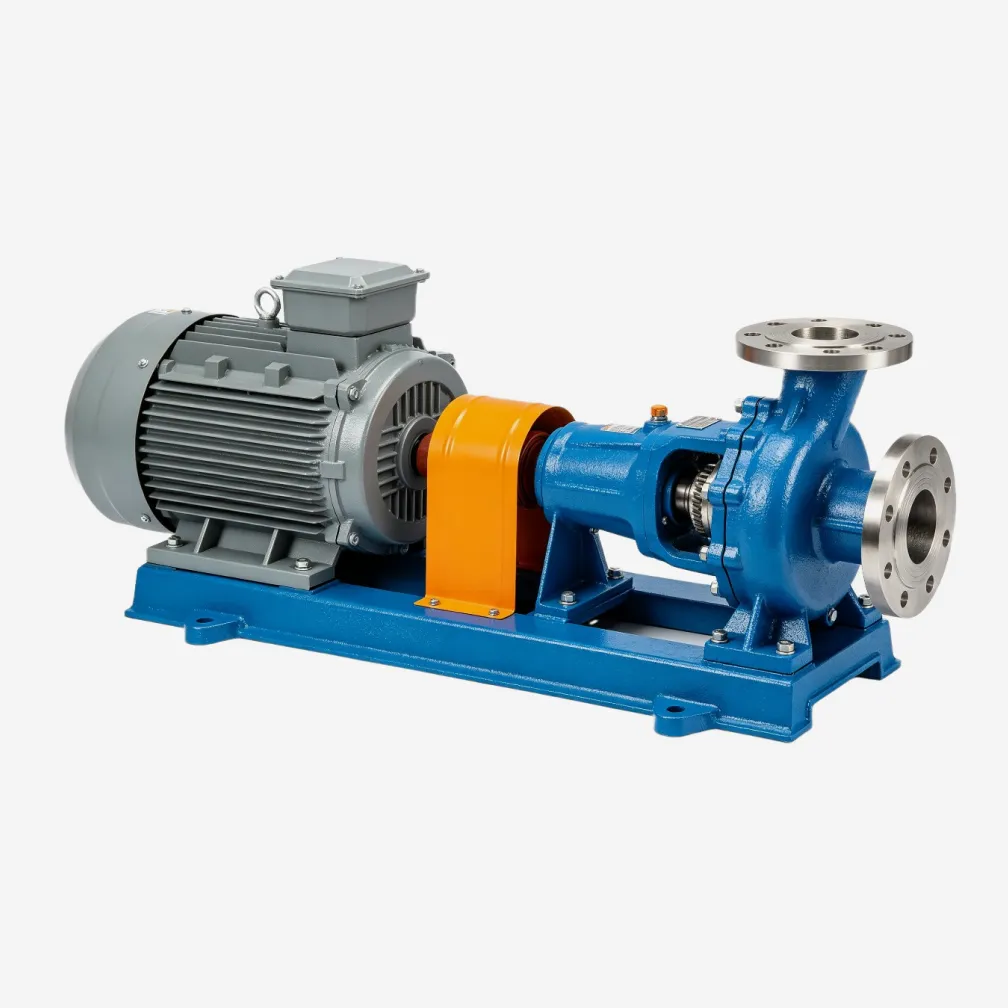
The IH stainless series uses a back pull-out design, so ensure enough clearance at the rear to withdraw the motor and bracket without disturbing the casing or piping.
Piping loads
Pipe flanges must align to the pump nozzles naturally, without springing them into position.
Excess piping load distorts the casing, accelerates seal wear, and can crack a fluoroplastic lining at the flange.
Support independent piping near the pump so the pump carries no pipe weight.
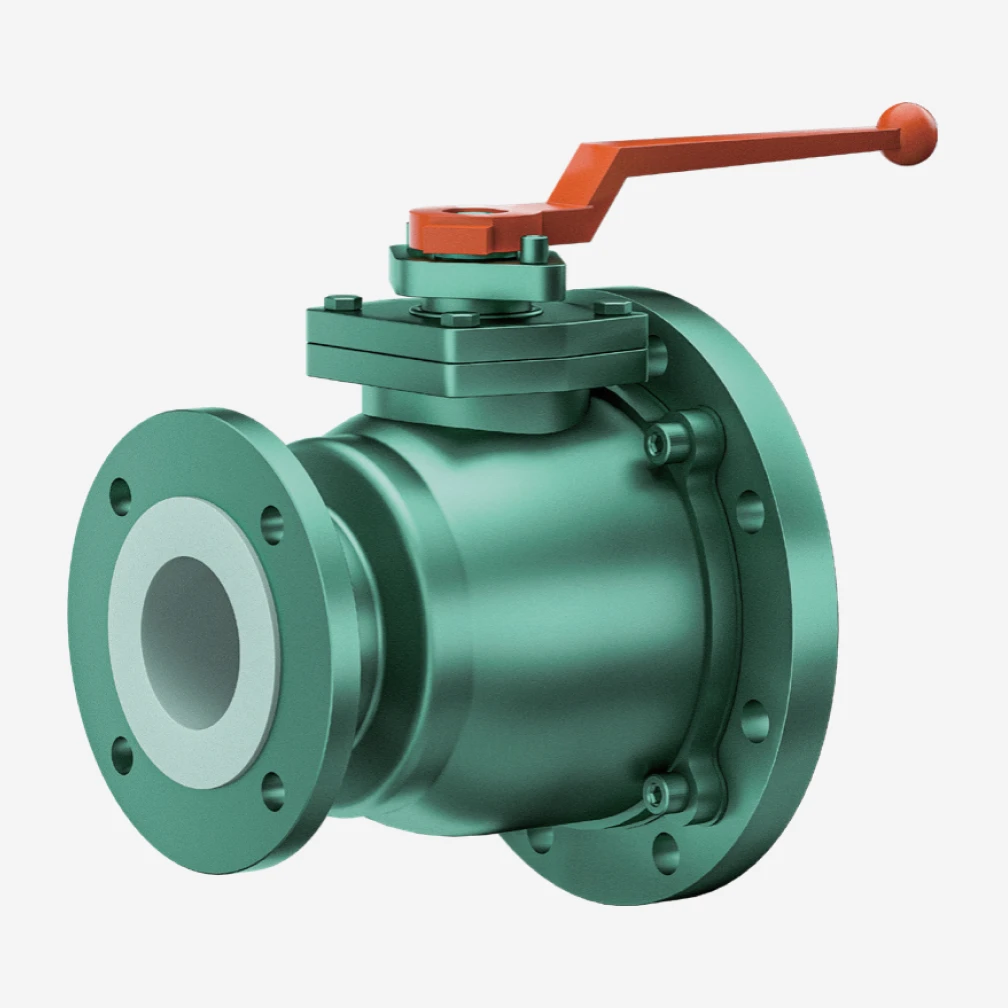
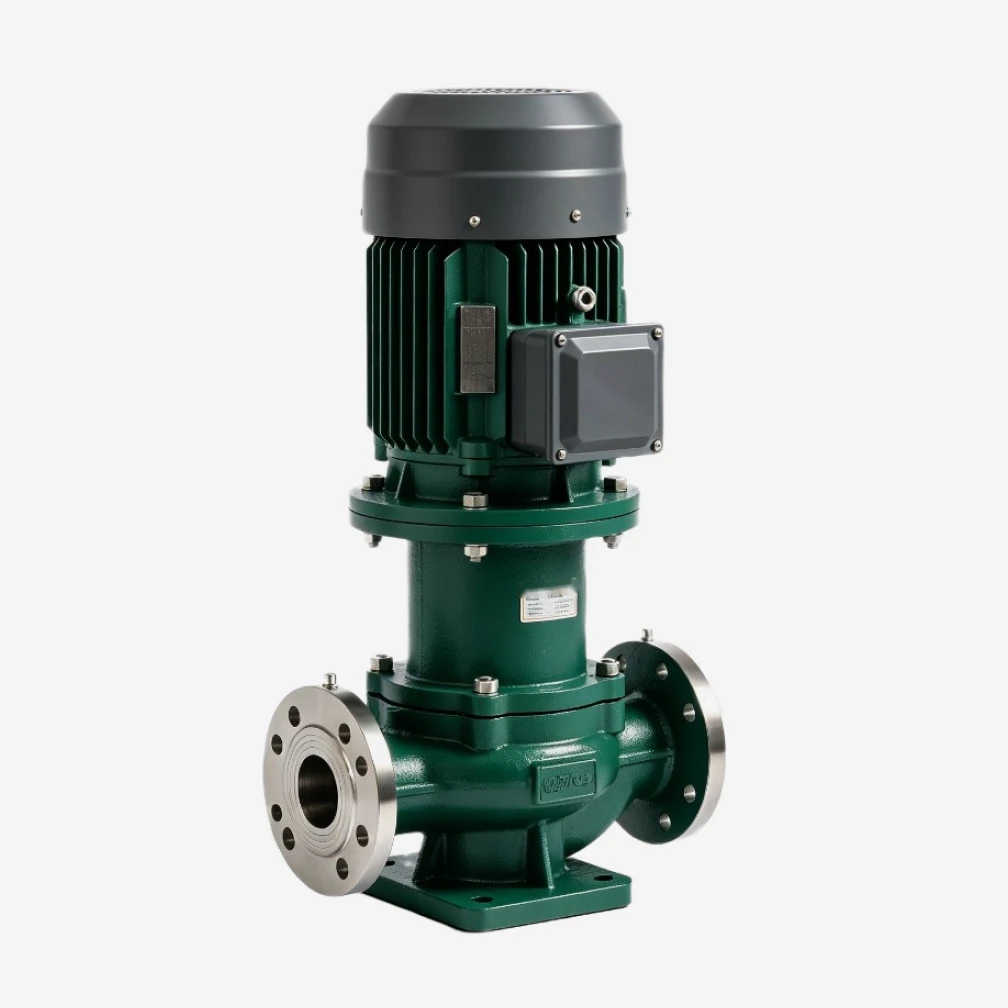
Use matched fluoroplastic-lined valves, pipes and fittings (PN10/PN16, ANSI 150) so flange standards and facing align with the pump.
Alignment
Dial-indicator or laser-align the pump and motor shafts, then re-check after grouting cures and after the first heat-up.
Correct for hot alignment if the pump runs warm.
Re-verify alignment periodically; misalignment is the leading cause of premature bearing and seal failure.
Startup and Commissioning
Before first energising any chemical pump, complete these commissioning checks:
Priming
Never start a standard centrifugal pump dry.
Fill the casing and suction line completely with the process liquid (or a compatible flush).
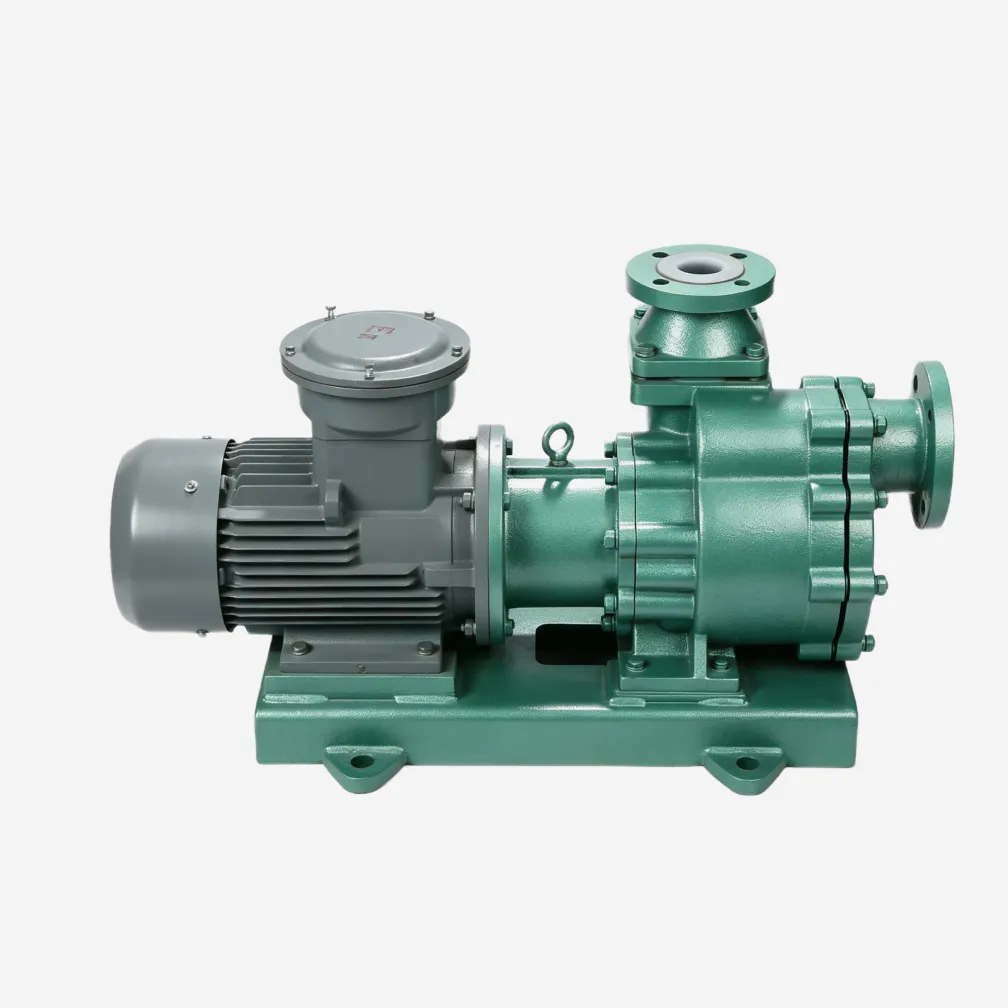
Self-priming pumps (FZB, ZMD, ZCQ) are primed once at first use; thereafter they re-prime automatically, but they must still retain enough liquid in the reservoir.
Rotation check
Bump the motor and confirm rotation direction matches the arrow on the casing.
Reverse rotation delivers little or no flow and can unscrew impeller nuts.
Valve sequence
Open the suction valve fully, close or crack the discharge valve, then start.
Open the discharge valve gradually to the duty point to avoid starting against closed head (or fully open, depending on motor starting capacity).
Seal/flush verification
For flushed or double mechanical seals, confirm barrier/flush fluid is flowing and at the correct pressure before introducing process liquid.
For magnetic-drive pumps, confirm the pump is vented and full of liquid, since dry starting destroys the sleeve bearings.
First-run checks
Within the first minutes verify no leakage, acceptable vibration, correct discharge pressure, and stable motor amperage below nameplate.
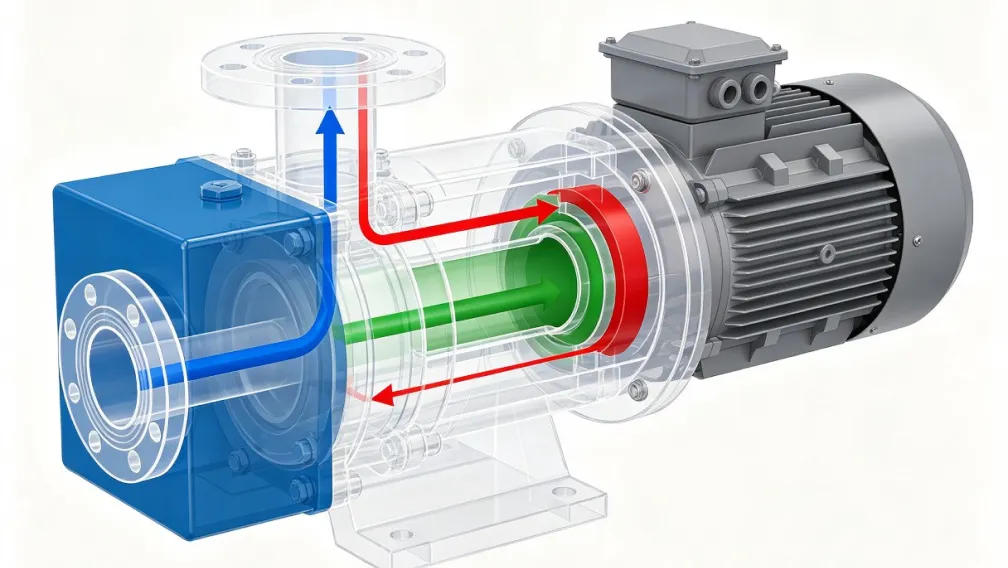
Magnetic-drive pumps are unforgiving of dry running.
Their internal sleeve bearings are lubricated by the pumped liquid, and the isolation sleeve depends on liquid flow for cooling.
Even a few seconds dry can scorch the sleeve and bearings.
Verify prime before start, every time.
Routine Inspection Schedule
Establish a layered inspection cadence so small problems are caught before they become failures.
Daily Checks
Listen for changes in noise (cavitation, rubbing, bearing whine).
Check for leakage at the mechanical seal, flanges, and isolation sleeve area.
Confirm discharge pressure and motor amperage are within normal bands.
Verify bearing/motor housing temperature by touch or sensor (flag anything trending up).
For flushed/double seals, confirm barrier-fluid level and pressure.
Weekly Checks
Inspect for vibration trends; log a reading at a marked bearing point.
Check mechanical seal flush lines for blockage or flow restriction.
Visually inspect baseplate grout and hold-down bolts for looseness.
For magnetic pumps, inspect the isolation-sleeve area for heat discoloration.
Walk all process-side fluoroplastic-lined piping/valves for weeping at flanges.
Monthly Checks
Re-check pump-to-motor alignment and correct if drifted.
Lubricate bearings per the schedule (grease gun to marked fittings; do not over-grease).
Verify the duty point is still near the best-efficiency point, since system changes erode this over time.
Sample and inspect barrier fluid for contamination (double seals).
Record any seal leakage trend; plan face replacement if increasing.
Mechanical Seal Care
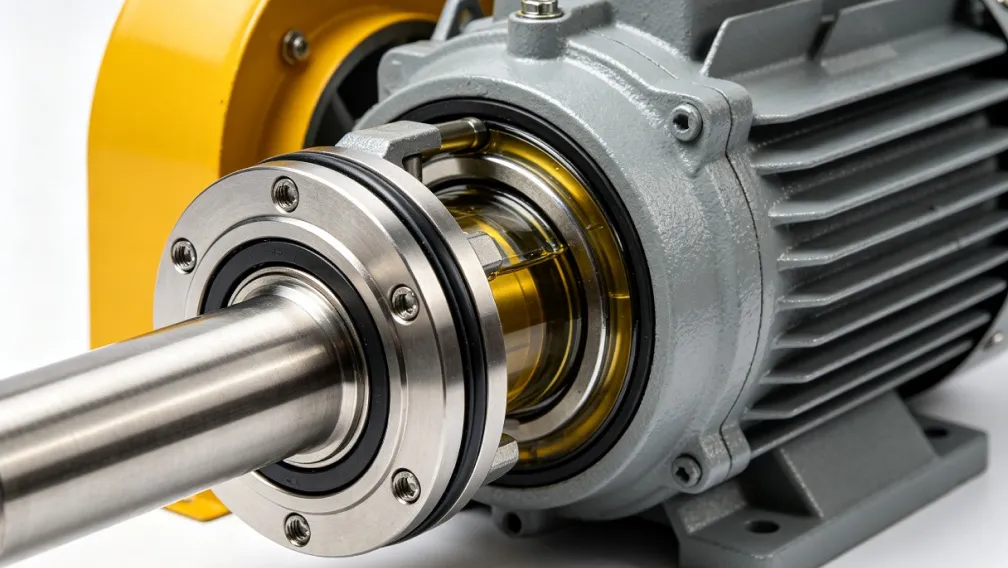
The mechanical seal (IHF, FSB, FZB, IH, UHB-ZK) is the highest-wear precision component.
Its care determines leak-free life.
Flush plans
Ensure the configured API flush plan (e.g. clean flush from discharge, or external clean barrier) is actually flowing and not blocked.
A blocked flush lets the seal faces run dry and overheat.
Barrier fluid (double seals)
Maintain barrier-fluid pressure above the process pressure so any leakage is barrier-to-process, not process-to-atmosphere.
Top up and sample barrier fluid regularly; replace if contaminated.
Face replacement
The 99.9% alumina-ceramic/silicon-nitride stationary and PTFE-filled rotating faces are consumables.
Replace them as a set at the first sign of steady visible leakage, or on a planned interval (typically annually for continuous duty).
Never lap a worn PTFE-filled face; replace it.
Avoid solids
If the medium carries solids that the flush cannot exclude, the faces will abrade rapidly; consider moving to a magnetic-drive pump or a slurry-duty seal.
Magnetic-Drive Bearing & Isolation-Sleeve Care
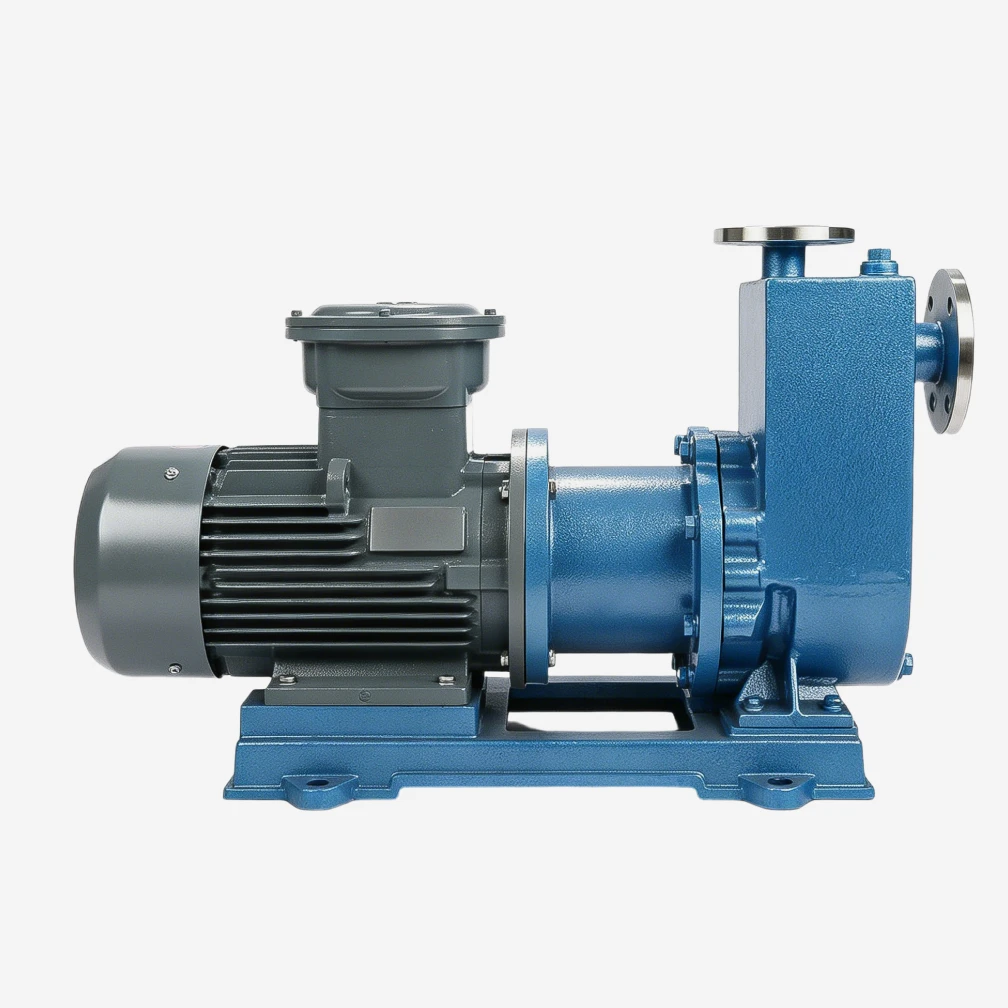
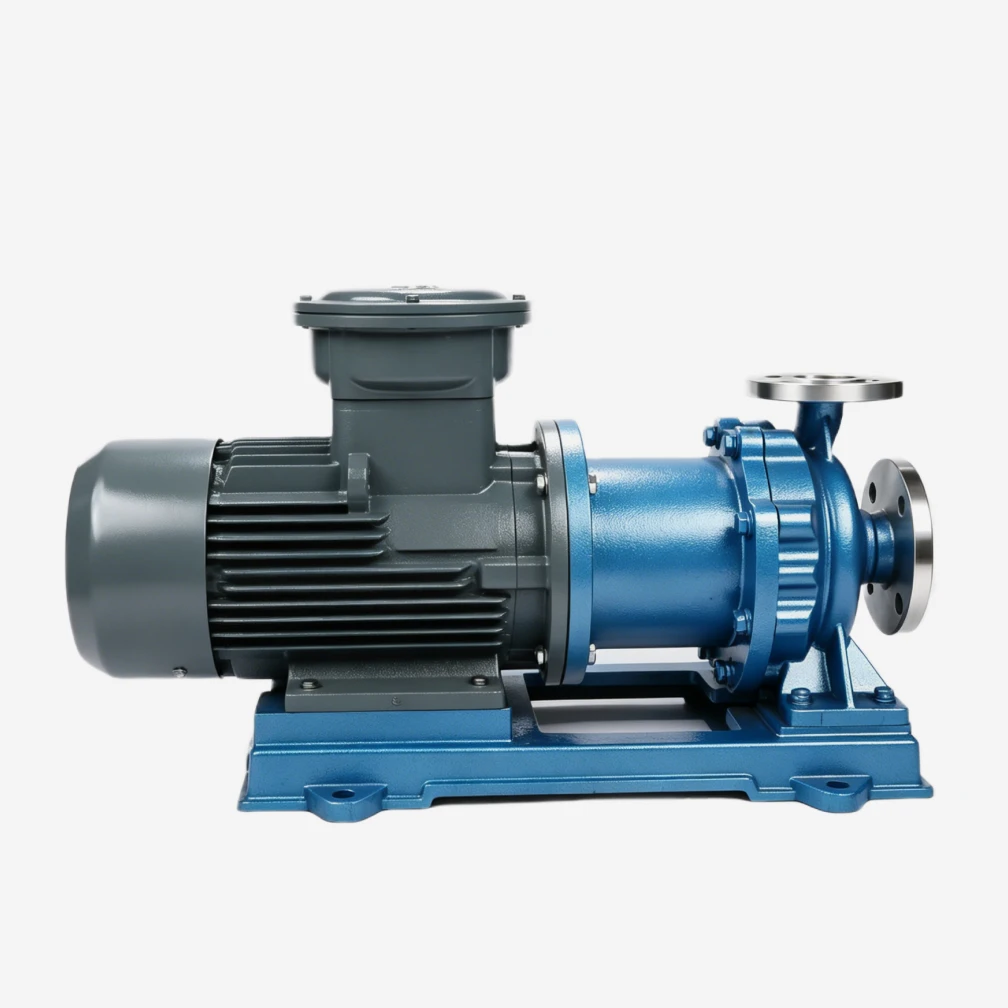
Magnetic-drive pumps (CQB, CQL, ZMD, ZCQ) trade the dynamic seal for internal sleeve bearings and an isolation sleeve that need their own discipline.
Keep it wet
The sleeve bearings (often silicon carbide in the ZMD) rely on the pumped liquid for lubrication and cooling.
Dry running destroys them almost instantly.
Isolation sleeve inspection
The ZMD uses an all-plastic isolation sleeve to avoid magnetic eddy currents and heat loss; check it for heat damage, cracking, or swelling during outages.
Metal-sleeve magnetic pumps (CQB, CQL) can develop eddy-current heating if run with the wrong liquid conductivity, so monitor temperature.
Decoupling watch
If the inner and outer magnets slip (decouple) under excessive torque or viscosity, the pump stops pumping while the motor runs.
Shut down immediately, let magnets cool, identify the overload (viscosity, solids, blocked line), clear it, and restart.
Repeated decoupling magnetises and weakens the coupling permanently.
Bearing clearance
During overhaul, measure shaft radial play; excessive play indicates worn sleeve bearings; replace before the impeller contacts the casing lining.
Lining Inspection (Fluoroplastic & UHMWPE)
Linings are the sacrificial barrier protecting the metal housing; they must be monitored for thinning and damage.
Fluoroplastic (F46/PTFE/PFA)
During outages, inspect the casing bore and impeller for:
lining discolouration
blistering
cracking
pinholes
local thinning
Pay particular attention to the volute cutwater and impeller eye where velocity and turbulence are highest.
Any pinhole means the metal housing is now exposed; schedule relining before return to service.
UHMWPE (UHB-ZK)
The 8–20 mm lining is designed to wear.
Gauge its residual thickness at high-wear zones (volute, impeller shroud) and record the trend.
Plan relining when thickness approaches a minimum (commonly around half of original), well before the steel housing is approached.
Flange faces
Inspect lining flange-face turnout (the lining that folds over the flange face to seal) for damage from overtightened or misaligned flanges.
This is a common leak path on lined pumps and valves.
Never weld, burn, or flame-torch near a lined pump: local heat destroys the lining from the inside.
Lubrication
Use only the grease/oil grade specified by the manufacturer; mixing incompatible greases causes breakdown.
For grease-lubricated bearings, follow the relubrication interval and quantity; over-greasing raises bearing temperature and blows seals.
For oil-bath bearings, maintain the oil level at the marked line; change oil at the prescribed hours or annually, whichever comes first.
Magnetic-drive pumps have no shaft-penetration bearing to grease; their sleeve bearings are liquid-lubricated (see above).
Spare Parts Strategy
A planned spares inventory converts an unplanned failure into a short outage.
Prioritise
Always in stock:
One complete set of mechanical-seal faces (or a cartridge seal assembly)
All O-rings/gaskets for the wetted end
For magnetic pumps:
A spare set of sleeve bearings
A spare isolation sleeve
For lined pumps:
A spare impeller
Where practical, a spare lined casing or relining kit, since lining lead times are long
For slurry pumps:
A spare impeller (open and/or closed type)
Front/rear wear liners
Common consumables:
Bearings
Lip seals
Coupling elements
Gasket sets
Fasteners
Store spare fluoroplastic-lined and UHMWPE components flat, out of direct sunlight and away from heat, to prevent lining distortion and ageing during storage.
Seasonal & Annual Maintenance Table
| Interval | Maintenance Task | Applies To |
|---|---|---|
| Daily | Noise/leak/pressure/temperature walk; barrier-fluid check | All pumps |
| Weekly | Vibration log; flush-line flow; base/bolt check; sleeve heat check | All pumps |
| Monthly | Re-alignment; lubrication; duty-point review; barrier-fluid sample | All pumps |
| Quarterly | Seal leakage trend review; coupling element inspection | Sealed pumps |
| Quarterly | Isolation-sleeve visual; bearing-clearance spot check | Magnetic-drive pumps |
| Quarterly | Slurry impeller & liner thickness gauging | UHB-ZK slurry pump |
| Annually | Full outage: replace seal faces (continuous duty); bearing inspection/replacement; full lining thickness survey and pinhole inspection | All pumps |
| Annually | Replace sleeve bearings & inspect/replace isolation sleeve; demagnetise-coupling check | Magnetic-drive pumps |
| Annually | Re-bed/re-grout baseplate if voids found; re-verify hot alignment | All pumps |
| Pre-winter (cold-climate) | Drain and protect idle pumps against freezing; verify heat tracing on flush/barrier lines | Idle / outdoor pumps |
| Pre-summer | Confirm cooling provisions (barrier-fluid cooler, motor fan) for peak temperature duty | High-temp / continuous pumps |
Troubleshooting & Related Guides
When a fault does appear despite good maintenance, the Troubleshooting Guide maps symptoms to causes and corrective actions.
To confirm you started with the correct material and model, revisit the Material Guide and Selection Guide.
© Youfu Lanke (优氟蓝科) · Corrosion-resistant chemical pumps · cnchemicalpump.com
Part of the Resources knowledge series: Knowledge Base · Selection Guide · Material Guide · Maintenance Guide · Troubleshooting.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.