
 English

Lubrication Failure Is the Fastest Route to Bearing Failure
Rolling-element bearings in pump service are designed for long life, commonly rated in tens of thousands of hours, yet field failures arrive far earlier, and lubrication sits behind the majority of them. The failure modes are specific: wrong lubricant, wrong quantity, wrong interval, and contamination. Each one is a maintenance-process failure rather than a component defect, which means each one is preventable with discipline rather than expense. Chemical pumps add their own pressures: corrosive atmospheres attack seals and degrade lubricants, washdown and humidity drive water into housings, and high process temperatures push oils toward their limits. This guide covers the three lubrication regimes found across chemical pump designs, grease, oil bath, and process-liquid lubrication, with the practices that keep each one working.
What the Lubricant Actually Does
The lubricant's job in a pump bearing is more than friction reduction. It forms the film that separates rolling elements from raceways, carries heat away from the contact zone, excludes contaminants at the bearing seals, and protects metal surfaces from corrosion during standstill. Every lubrication failure maps to one of these functions breaking down: too little grease starves the film, too much grease churns and overheats, aged oil loses film strength, and water in the oil attacks the raceways directly. Keeping the functions in mind turns lubrication from a calendar task into a condition discipline.
Grease Lubrication: The Discipline of Quantity
Selection
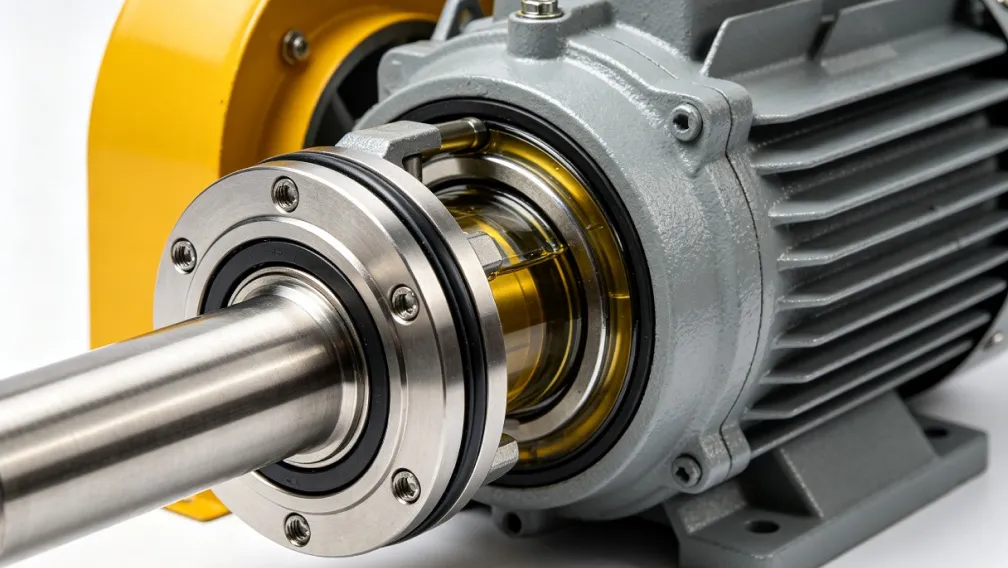
Use the grease grade specified by the pump manufacturer, and treat mixing as a fault. Greases are oils held in thickener matrices, and incompatible thickener systems, mixed in the same bearing, can soften, harden, or separate, destroying the lubricant's structure without any visible warning at the grease gun. Where a change of grease grade is genuinely required, the bearing is cleaned out completely during an outage rather than topped over. For chemical plant atmospheres and humid environments, the specified grade typically carries corrosion inhibitors and water resistance; substituting a generic multipurpose grease quietly removes both.
Quantity and Interval
Over-greasing is as destructive as neglect, and far more common. A bearing packed beyond its designed fill has nowhere for the grease to move; the rolling elements churn it continuously, friction heat builds, temperature climbs, and the excess pressure blows out the bearing seals, opening the door to the contamination the seals existed to stop. The correct practice is measured: relubricate at the manufacturer's interval with the manufacturer's quantity, delivered slowly through the marked fitting, and where the design provides a drain or relief, remove the plug during greasing so spent grease can escape. Record each relubrication in the pump log; the interval belongs to the pump's duty and temperature, and the log is what keeps the schedule honest across shift changes.
Oil Bath Lubrication: Level, Condition, and Change
Larger bearing frames run in an oil bath, where the lubricant also carries most of the bearing's heat load. Three disciplines govern it. Level comes first: the oil level sits at the marked line on the sight glass, checked on a standing pump, because an overfilled bath churns and overheats exactly like an over-greased bearing, while a low level starves the lower rolling elements. Condition comes second: oil darkens, emulsifies with water, and accumulates wear particles in service, and a monthly look at the sight glass catches all three before they reach the raceways. Milky oil means water ingress, and the response is an oil change plus a hunt for the entry path, usually a worn lip seal or a breather pulling in humid air. Change interval comes third: replace the oil at the prescribed operating hours or annually, whichever arrives first, with the specified viscosity grade. On hot duties the interval shortens, because oxidation rate roughly doubles with every 10°C of operating temperature, and oil that has oxidized loses film strength before it looks bad.
The breather deserves mention because it is small and decisive. A clogged or missing breather lets the housing pressure cycle with temperature, pumping moist air in and out past the seals. Checking the breather at every oil check costs seconds and removes the most common water ingress path.
Process-Liquid Lubrication: The Sealless Case
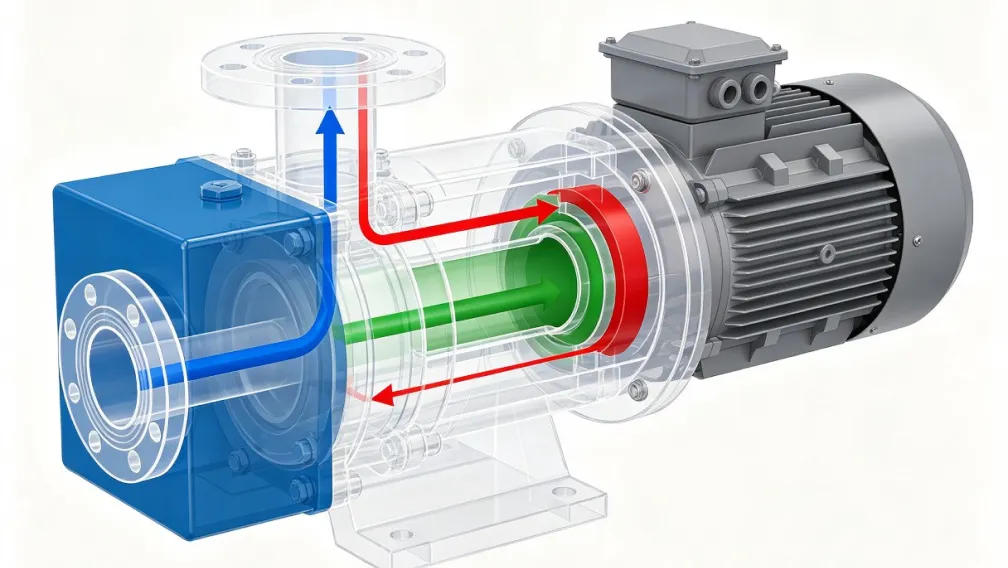
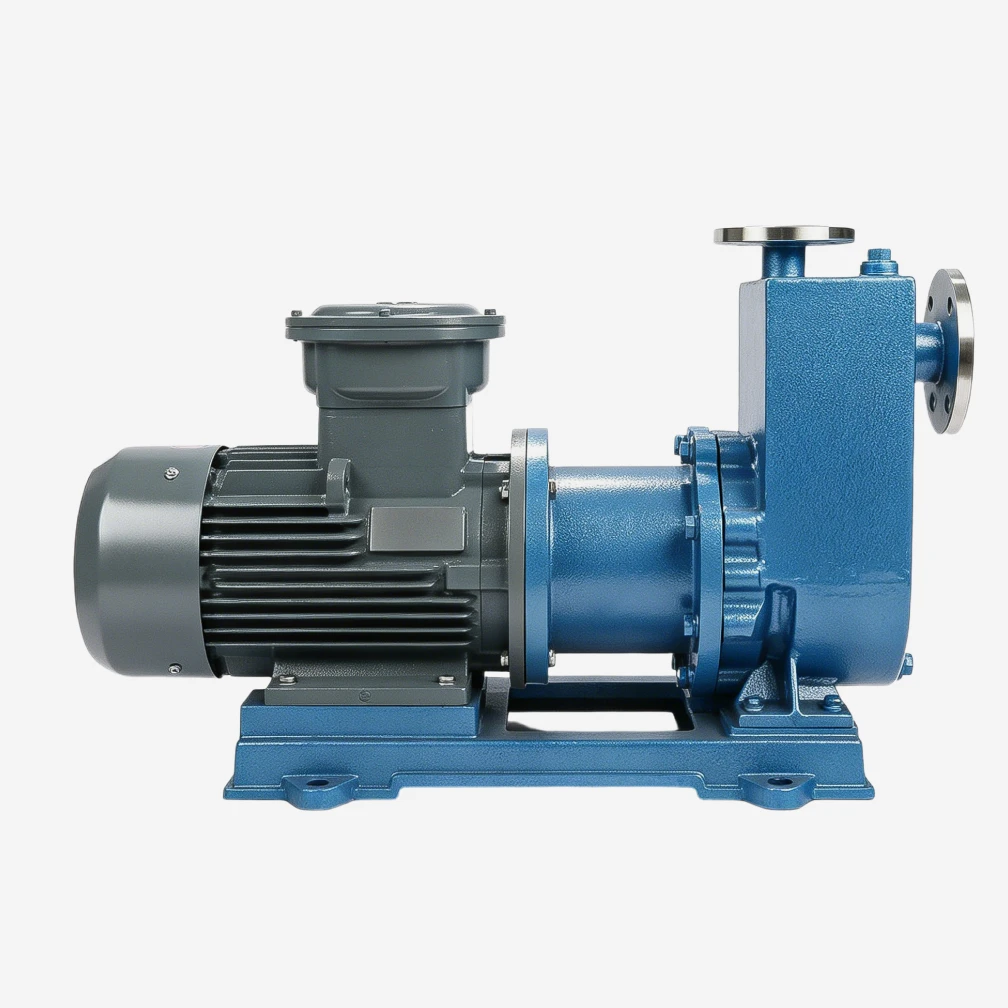
Magnetic drive pumps carry no shaft-penetration bearings to grease or oil. Their internal sleeve bearings, typically silicon carbide, are lubricated and cooled by the pumped liquid itself, circulated through the bearing housing by the pump's internal pressure balance. This eliminates the lubrication schedule entirely and replaces it with three operating disciplines. The pump must never run dry, because the liquid is the lubricant and a few seconds without it scorches the bearings. The fluid feeding the bearings must stay clean, because abrasive particles in the internal circulation grind the sleeves, which is why inlet strainers on dirty services are a lubrication measure. And the internal clearances must be measured at overhaul, since sleeve bearing wear shows as growing shaft play rather than as any external lubricant symptom. On a fluoroplastic magnetic drive pump in clean corrosive service, this regime routinely outlasts every oil and grease schedule in the plant, with nothing to replenish and nothing to contaminate.
Contamination Control at the Point of Application
More abrasive enters bearings through the grease gun than through any seal. The fitting, the gun coupler, and the grease itself are all contamination paths, and each has a simple control. Wipe the fitting and coupler clean before every connection; the grit sitting on an unwiped fitting is injected directly into the bearing under grease gun pressure. Keep grease gun caps on between uses, and store cartridges and oil containers sealed, indoors, and off the floor, because open containers collect dust and condense water. Use dedicated transfer equipment for each lubricant type rather than shared pumps and cans, which mix grades and carry debris between products. And treat the first pump of a grease gun with suspicion: grease sitting in the nozzle between uses collects contamination, so a small purge onto a rag before connecting costs a gram of grease and protects a bearing rated for tens of thousands of hours.
Reading the Bearing's Condition Signals
Lubrication problems announce themselves before failure if the signals are read. Temperature is the primary indicator: a bearing housing trending upward week over week is reporting a lubrication or condition problem, and the daily touch check plus monthly instrumented reading is the monitoring baseline. Noise adds detail: a smooth hum is healthy, a rising whine suggests film breakdown, and a rough or intermittent rumble suggests damaged raceways. Vibration trending catches what the ear misses, with lubrication faults typically appearing as a broad rise in high-frequency energy well before the classic bearing defect tones. Oil analysis, where the population justifies it, closes the loop by measuring viscosity, water content, and wear metals directly. The common thread is trending: every one of these signals is meaningful against the pump's own history and nearly meaningless as a one-off reading.
Lubrication Practices That Prevent the Common Failures
| Practice | Failure prevented |
|---|---|
| Manufacturer-specified grease, never mixed | Thickener incompatibility, lubricant breakdown |
| Measured grease quantity at marked intervals | Churning, overheating, blown bearing seals |
| Oil level at the marked line, standing pump | Starvation or churning in oil bath frames |
| Monthly oil condition check; annual change | Oxidation, water emulsion, wear-particle damage |
| Breather checked at every oil check | Moisture ingress through pressure cycling |
| Clean fittings and grease gun before use | Abrasive contamination injected with lubricant |
| Temperature and vibration trended, not spot-read | Late detection of film breakdown and wear |
Conclusion
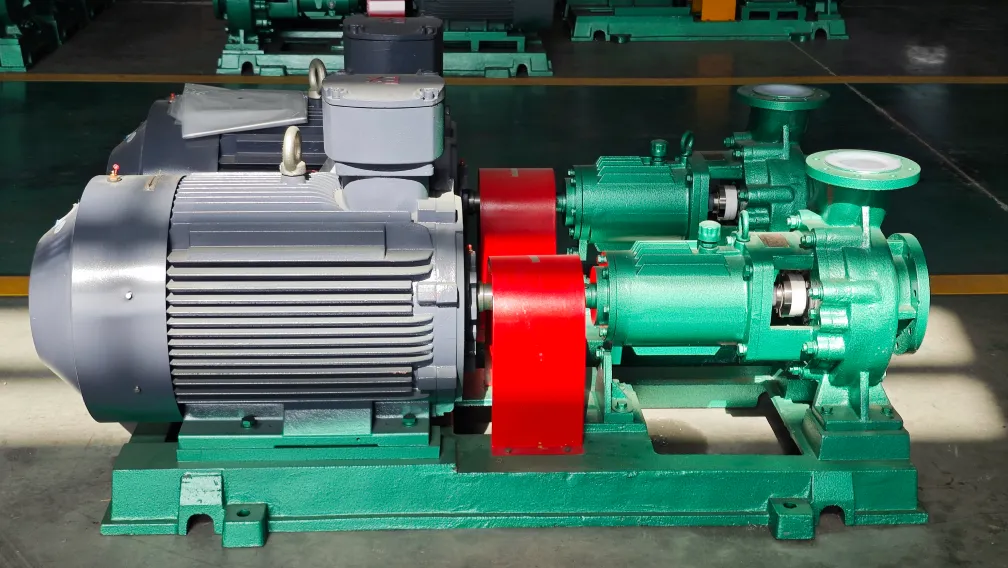
Bearing lubrication in chemical pump service is a condition discipline applied to three regimes: grease systems that demand measured quantity and unmixed grades, oil baths that demand correct level, clean oil, and working breathers, and process-liquid bearings in sealless pumps that demand clean fluid and zero dry running. The common causes of premature bearing failure, over-greasing, water ingress, oxidized oil, and contamination, are all process failures with procedural fixes. YFTEL specifies lubricant grades, quantities, and intervals in every pump manual across the sealed centrifugal chemical pump and magnetic drive ranges. Send us your operating temperatures and environment, and our engineers will confirm the lubrication specification and interval for your conditions.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.