
 English

Flow Problems Are System Problems First
Of all pump complaints, "it's not pumping" generates the most unnecessary disassembly. The instinct is to open the pump, yet the majority of no-flow and low-flow faults live outside the casing: a closed valve, an air pocket, a blocked strainer, a reversed motor. The pump is simply the component that reports the system's problem. Effective diagnosis works a fixed sequence: verify the priming state, verify the rotation, verify the suction path, verify the system demand, and only then inspect the pump's internals. This guide works that sequence for the three related symptoms, no flow at startup, low flow, and low discharge pressure, which share most of their causes and all of their diagnostic logic.
Before Anything Else: Safety and Evidence
The preparation does not change with the symptom. Isolate the pump electrically with lockout and tagout, close the suction and discharge valves, and depressurize, drain, and flush the casing before opening anything wetted. Then gather the evidence that costs nothing: the discharge gauge reading, motor current against nameplate, the sound of the pump, and the history. A pump that lost flow gradually over months is reporting wear; one that stopped after a shutdown, a valve operation, or a batch change is reporting that event. The evidence halves the cause list before a wrench is lifted.
Symptom Patterns That Name the Cause
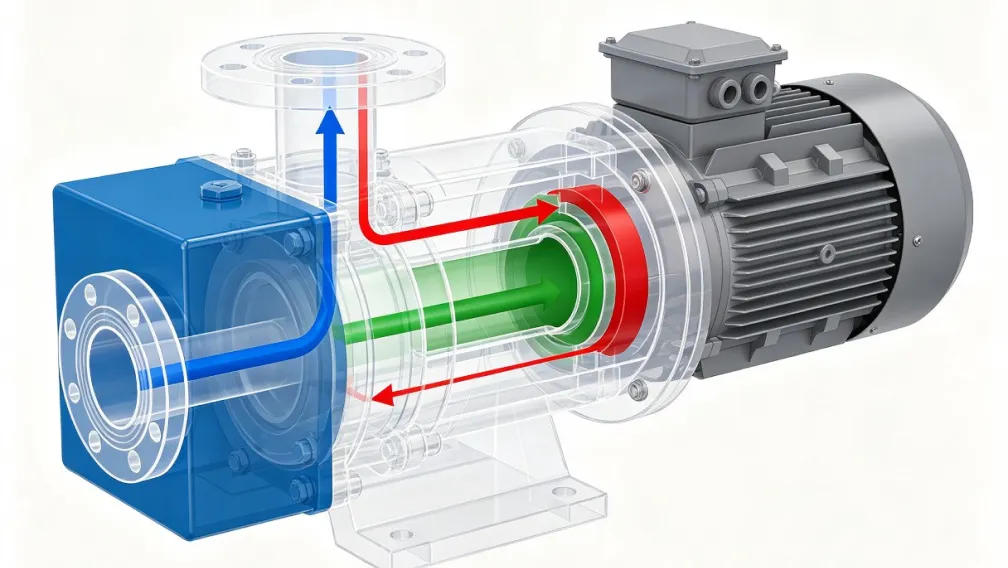
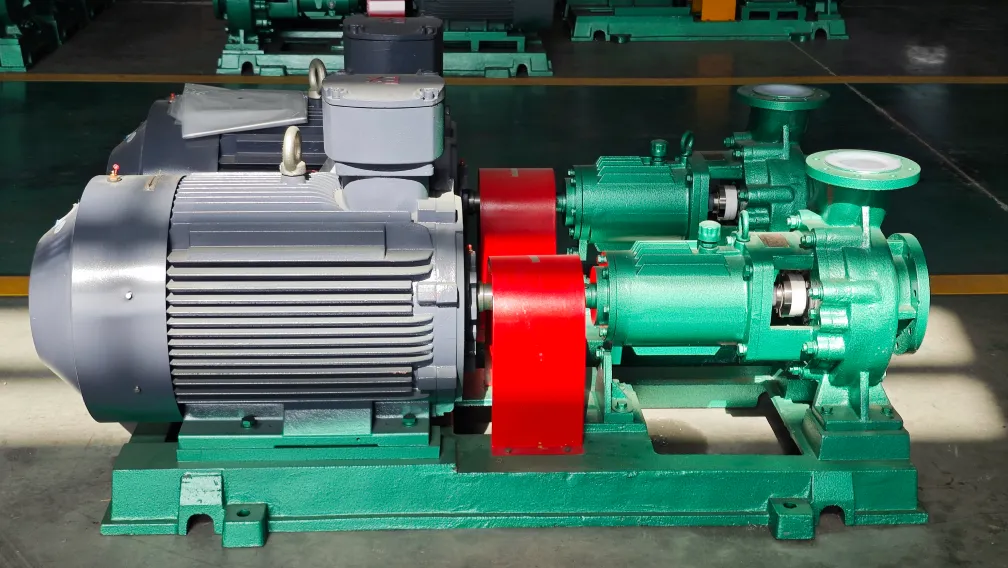
The way flow failed carries as much information as the failure itself, and four patterns account for most cases. No flow at startup, on a pump that has never run or has just been opened, points to priming, rotation, or a closed valve: the commissioning errors, in order. Sudden loss of flow in a running pump points to an event: the source ran dry, a suction joint let go, a blockage arrived from upstream, or on a magnetic drive pump, the coupling decoupled under overload, in which case the motor runs unloaded and the flow stops while the machine sounds almost normal. One configuration note for magnetic drive pumps: because the motor keeps running when the coupling decouples, motor current falls sharply at the moment flow stops, and a current trend makes the diagnosis immediate. Gradual decline over weeks or months is the wear signature: impeller erosion, widening clearances, or a strainer loading progressively, and it is read against the maintenance log's pressure and current trends. Intermittent flow, surging and recovering, points to air: a vortexing sump at low level, an air leak that admits more as the level falls, or a fluid releasing dissolved gas at the impeller eye. Read the pattern first, and the five-step sequence starts at the right step instead of the first one.
Step 1: Verify the Priming State
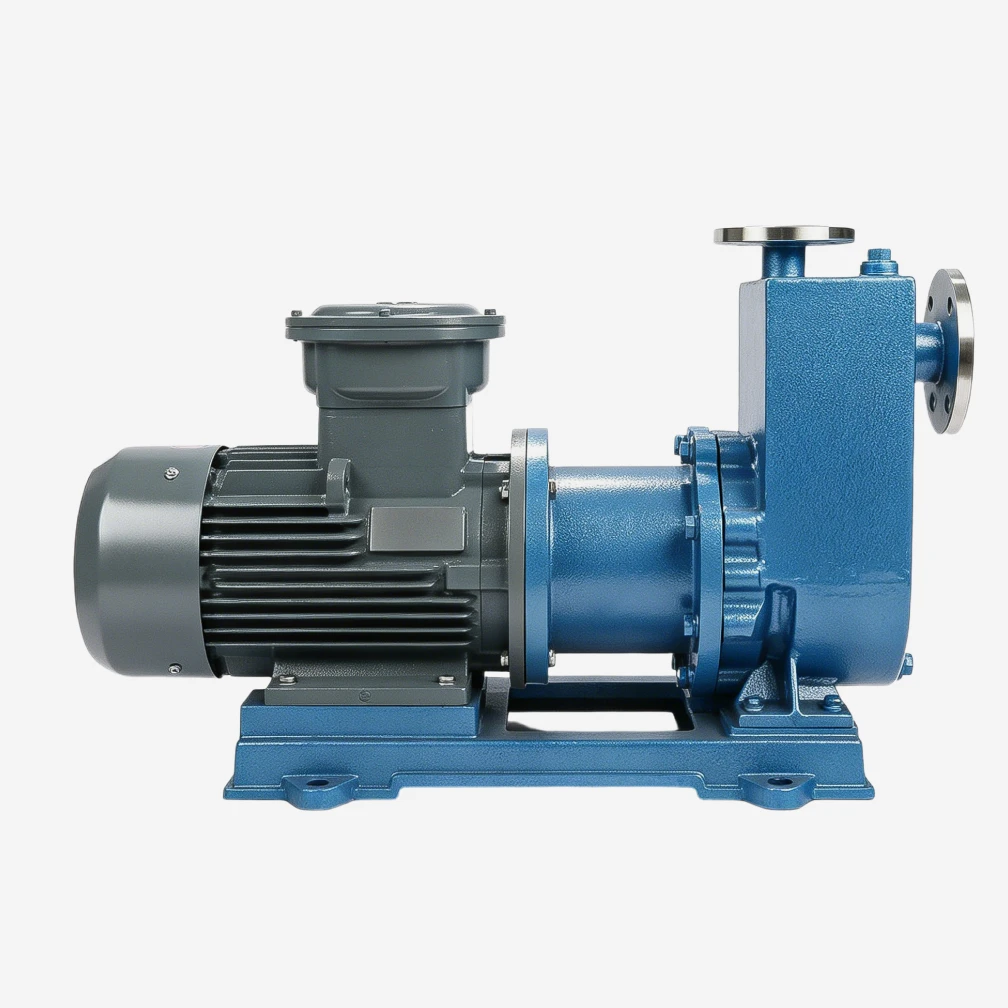
A centrifugal pump pumping air delivers nothing, and priming faults are the leading cause of no-flow at startup. Confirm the suction valve is fully open and the casing is filled and vented: crack the vent at the casing high point until liquid appears without bubbles, since trapped air collects exactly where the seal sits. On self-priming pumps, confirm the reservoir still holds its charge; a casing drained by a leaking check valve or a long shutdown primes nothing until it is refilled once by hand. If the pump was running and lost flow, suspect a suction source that ran dry or an air leak that finally outpaced the pump.
Step 2: Verify Rotation
Reversed rotation delivers a fraction of rated flow and pressure, and on designs with threaded impeller retention it can unscrew the impeller nut within seconds. The check takes ten seconds: with the coupling element removed, bump the motor and watch the shaft against the arrow on the casing. Reversed rotation after maintenance usually means two phases swapped during reconnection, which is why this check belongs to every startup, not just the first one.
Step 3: Clear the Suction Path
The suction side owns most flow problems, and its faults share one mechanism: the pump is starved. Work the path from source to impeller. Confirm the source level is above the minimum and the suction valve fully open. Inspect the strainer, because a strainer clogging progressively is the classic slow loss of flow. Check the suction lift against the pump's rating, derated for the fluid's actual density, since a lift that worked on water data may exceed what a denser fluid allows. And hunt for air ingress: a self-priming or lifted-suction pump that pulls air through a loose flange, a perished gasket, or a valve stem will happily pump that air instead of liquid, and the symptom looks exactly like a pump fault. Tighten, replace, and re-test before suspecting the pump.
Step 4: Check What the System Is Demanding
A pump delivers what the intersection of its curve and the system curve allows, and systems change. A discharge valve throttled further than designed, a filter loading up downstream, a new branch added to the line, or a level difference that grew, all raise the system head and push the operating point left, cutting flow and pressure without anything being wrong with the pump. Compare the actual installation against the design: valve positions, downstream restrictions, and the true static levels. Then check the motor speed and supply voltage, because a motor running slow, wrong frequency, wrong pulley, or a failing winding, moves the entire pump curve down. Cavitation belongs to this step as well: partial cavitation reduces flow and pressure before it becomes clearly audible, and its gravel-like rattle confirms it.
Step 5: Inspect the Pump Internals
Only with the external causes eliminated does the pump itself become the suspect, and the internal causes of low flow form a short list. Impeller wear is the common one: eroded or corroded vanes move the whole performance curve downward, and gauging the impeller diameter and eye clearance against specification settles it. On lined pumps, lining wear at the impeller eye widens the internal clearances and lets flow recirculate internally instead of discharging. On slurry pumps, the same wear mechanism arrives faster and is tracked by the thickness gauging program rather than discovered by symptoms. A blocked or partially blocked impeller completes the list: stringy solids and crystallized deposits lodge in the passages and cut flow while the pump sounds nearly normal. Wear beyond limits means replacement or relining; blockage means clearing and an upstream screen to prevent recurrence.
The Diagnostic Sequence at a Glance
| Step | Check | Typical finding |
|---|---|---|
| 1 | Priming state: valve open, casing filled and vented | Air-bound casing; empty self-priming reservoir |
| 2 | Rotation against casing arrow | Two phases swapped at reconnection |
| 3 | Suction path: level, strainer, lift, air leaks | Clogged strainer; loose flange pulling air |
| 4 | System demand: valves, downstream restrictions, speed, cavitation | Throttled valve; loaded filter; slow motor |
| 5 | Internals: impeller wear, clearances, blockage | Eroded impeller; deposits in passages |
When Flow Problems Persist
A pump that passes all five steps and still underperforms is usually reporting a selection or system mismatch rather than a fault: the duty point has migrated from the design, the fluid properties differ from the specification, or the system curve has changed beyond what the pump can follow. At that point the productive move is to compare current operating data against the commissioning baseline and the original selection data. YFTEL engineers support exactly this analysis across the centrifugal chemical pump and magnetic drive ranges: send the symptom, the gauge readings, and the pump's history, and the diagnosis usually resolves without a site visit.
Conclusion
No flow and low flow are solved by sequence, not by disassembly: priming, rotation, suction path, system demand, and only then internals. Most cases resolve at the first three steps, with nothing opened but a vent plug and a strainer. Work the sequence, record what each step found, and the pump's flow problems stop being mysteries and start being maintenance items.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.