
 English

Overheating Is a Location Question First
"The pump is overheating" is the start of the diagnosis, and the first question is where the heat actually is, because a hot bearing housing, a hot pump casing, and a hot motor are three different problems with three different fix lists. Bearing heat is mechanical: friction at the rolling elements. Casing heat is hydraulic: the pump is churning liquid it cannot discharge. Motor heat is electrical or overload: the motor is converting too many amps into the load, or losing its ability to reject its own heat. Confusing them leads to the classic wasted repair, new bearings fitted to a pump that was dead-headed, or a motor rewound for an overload caused by a heavy fluid. This guide works through each location: the causes, the confirming checks, and the fixes.
Bearing Housing Heat: The Mechanical Cause
A bearing housing running hot has a short cause list. Lubrication failure leads it: oil level low or high, oil degraded or contaminated, grease over-packed so the bearing churns it, or the wrong lubricant grade for the temperature. Misalignment follows: pump and driver shafts offset or angled, forcing the bearings to carry cyclic loads they were never sized for, with the heat concentrated at the coupling end. Bearing wear itself is third: a bearing approaching the end of its life runs rough and hot, and the heat climbs as the damage progresses. The confirming checks are quick. Read the actual housing temperature and compare against the ambient plus normal rise; a housing you cannot keep a hand on is already in the action zone. Check the oil level and condition, listen at the housing with a probe, and verify alignment before assuming the bearing is the root cause. The fixes match the causes: correct the lubricant and its level, realign, and replace the bearing while naming what killed it, since a bearing replaced into the same misalignment lives the same short life.
Casing and Fluid Heat: The Hydraulic Cause
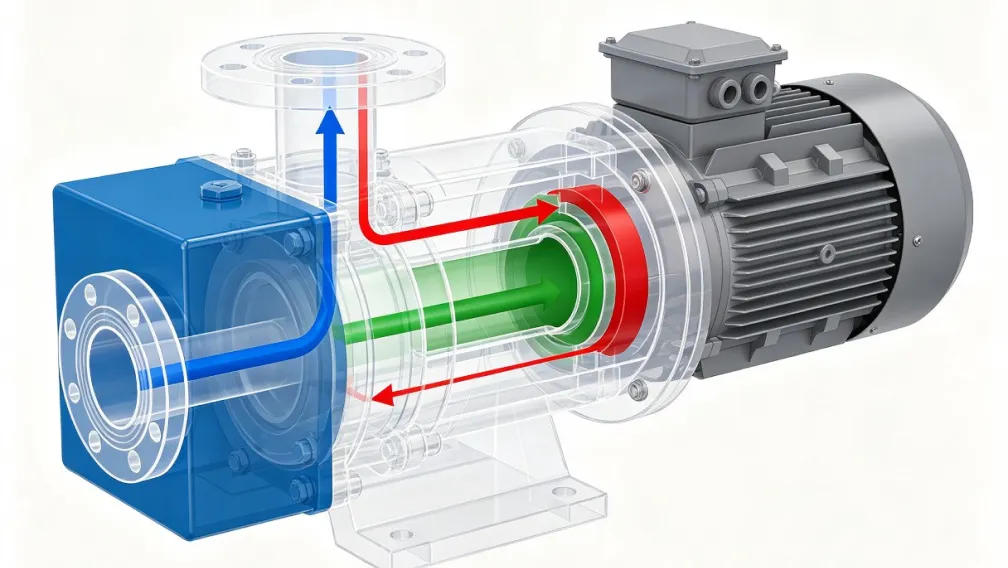
A pump casing that heats up is telling you the liquid inside is being worked without going anywhere. Every pump converts a share of its shaft power into fluid heat, and at normal flow that heat leaves with the stream. Close the discharge valve, throttle flow back to a trickle, or block the line, and the heat stays in the casing: the liquid churns through internal recirculation, the temperature climbs, and on chemical duty the fluid eventually vaporizes, the seal or bearings lose their lubricating film, and the pump is minutes from damage. This is why minimum flow limits exist, and why "the pump was only running against a closed valve for a little while" precedes so many seal and lining failures. The signature is a casing and discharge pipe warming steadily, a discharge gauge showing shutoff head, and flow at or near zero. The confirming check is simply the valve lineup and a flow reading. The fix is procedural: never run below the pump's minimum flow, fit a minimum-flow bypass where the process demands turndown, and interlock against closed-valve operation where the risk justifies it. On a lined chemical pump, add one more check after any overheating event: inspect the lining near the volute and seal chamber for deformation before returning the pump to service.
Motor Overload: The Hydraulic Causes
A motor drawing current above its nameplate full-load value is being asked for more power than the design intended, and the first suspects are hydraulic. Operation far right of the best efficiency point, run-out on the curve, raises absorbed power on a radial pump, and a worn or incorrectly sized system can push the duty there quietly as throttle valves open over time. Fluid heavier or more viscous than the design raises absorbed power directly: a pump selected for water-like duty and handed a fluid at 1.4 specific gravity asks its motor for forty percent more at the same point on the curve. An impeller trimmed too large, or replaced with the wrong trim during a past repair, overloads the motor at every operating point. The confirming checks are measurement: actual flow and head against the curve, actual fluid specific gravity and viscosity against the design data sheet, and impeller diameter against the record drawing. The fixes are to restore the duty point to the curve, correct the valve lineup that let the pump run out, or re-select the impeller trim or motor for the real fluid.
Motor Overload: The Mechanical and Electrical Causes
When the hydraulics check out, look mechanical and electrical. Mechanical binding raises load: an impeller rubbing the casing after a bearing failure or a bent shaft, debris jammed in the passages, or a coupling fitted tight enough to preload the shafts. Each shows up as current high at every flow, often with noise and vibration. Electrical causes imitate overload exactly: a lost phase leaves the motor running on two phases with current climbing and torque collapsing, low supply voltage raises current for the same power, and phase-to-phase voltage unbalance overheats windings even at moderate load. The confirming checks are electrical: measure current on all three phases, measure voltage at the motor terminals under load, and compare both against the nameplate. A current reading that differs between phases points electrical; a uniform high reading on all three points hydraulic or mechanical. The fixes sit with the electrician or the mechanic accordingly, and a motor that has tripped repeatedly on thermal overload deserves a winding check before it is asked again.
Reading the Ammeter: Overload Diagnosis at a Glance
| Current pattern | Likely cause | First check |
|---|---|---|
| High on all phases, rises with flow | Run-out on the curve | Flow and valve lineup vs design point |
| High on all phases at every flow | Heavy fluid, wrong impeller trim, or mechanical binding | SG/viscosity vs data sheet; impeller free rotation |
| Unbalanced between phases | Electrical supply problem | Voltage balance at motor terminals |
| Very high with motor struggling | Lost phase or seized rotating element | Supply phases; impeller by hand |
| Normal current, motor still hot | Cooling failure: blocked fan, dirty fins, hot room | Airflow over the motor |
Prevention: Trend the Two Cheap Instruments
Overheating failures almost never arrive unannounced; they arrive ignored. The two cheapest instruments on the pump, a thermometer or probe at the bearing housing and the ammeter on the motor, catch nearly every cause in this guide weeks before the trip. Log bearing temperature and motor current at the same load on a fixed schedule. A temperature trend climbing degree by degree is a lubrication or alignment problem developing. A current trend creeping upward is the duty drifting or the internals wearing. A reading that jumps is an event to investigate today. Plants that trend these two numbers rarely meet an overheating failure as a surprise.
The Restart Discipline
Overheated equipment earns a pause before any restart. A motor that tripped needs time to cool and a reason found; resetting a thermal trip without diagnosing the cause teaches the protection nothing and shortens winding life with every cycle. A pump that overheated hydraulically needs the fluid side inspected before it runs again: seals and linings checked for heat damage, bearings for film loss. And an overload traced to the process, a heavier batch, an opened valve, a changed recipe, needs the change recorded against the pump's data sheet, because the next overload will come from the same place. Where overloads recur seasonally or with specific batches, the pump and motor selection should be reviewed against the worst case the process actually presents, with margin, rather than the average case.
Conclusion
Overheating and overload are location questions first: find where the heat is, then work the short cause list for that location. Bearings overheat from lubrication and alignment, casings from flow that cannot leave, and motors from loads hydraulic, mechanical, or electrical, and the ammeter separates most of them in one reading. YFTEL engineers troubleshoot overload cases across the full range of centrifugal chemical pumps, from sealed process pumps to magnetic drive pumps and slurry pumps: send us the current readings, the duty data, and the fluid, and we will name the cause and the fix.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.